About MS Elevator Bucket Chain
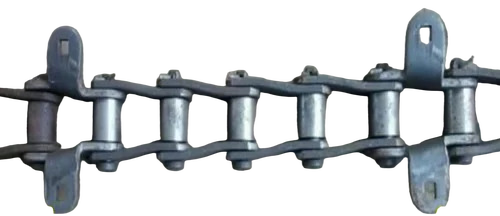
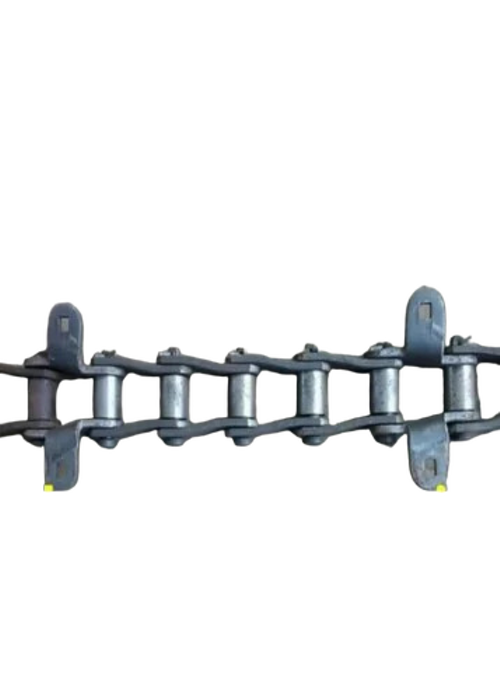
Presenting the MS Elevator Bucket Chain, a prodigious solution for heavy-duty bulk material handling. Crafted from mild steel and boasting a galvanized surface finish, this phenomenal chain delivers breathtaking corrosion resistance, making it ideal for use in rice mills, grain processing, and flour mills. Precision-engineered guide roller links ensure seamless operation and extended durability. Proudly manufactured, supplied, and exported from India, this chain combines affordability with unrivaled quality. Grab yours now to enhance your operational efficiency-order today and experience exceptional performance at a competitive rate!
Advantages and Commercial Applications of MS Elevator Bucket Chain
The MS Elevator Bucket Chain stands out for its high corrosion resistance and precision-engineered link pitch, making it a reliable choice in demanding environments. The direction of use typically involves vertical or inclined conveyance of bulk materials in rice mills, flour mills, and grain handling plants. Its heavy-duty capacity and robust construction provide a significant advantage for commercial material transport, ensuring smooth and efficient operations in industrial settings.
Supply Ability, Certifications, and FOB Port for MS Elevator Bucket Chain
With a strong supply ability, we efficiently fulfill bulk orders of MS Elevator Bucket Chains at an affordable rate. We provide full certification to guarantee product quality and compliance. Discuss your proposal amount directly with our experts for the best deal on large shipments. Transportation logistics are streamlined, as FOB shipments are available from top Indian ports, ensuring timely and secure delivery to your required location worldwide.
FAQ's of MS Elevator Bucket Chain:
Q: How is the MS Elevator Bucket Chain used in rice and flour mills?
A: The MS Elevator Bucket Chain is designed for the vertical or inclined conveyance of bulk materials like rice, grains, or flour. Its robust guide roller chain efficiently carries heavy loads within processing plants, supporting smooth and uninterrupted material flow.
Q: What are the core benefits of the galvanized surface finish?
A: The galvanized surface finish provides exceptional corrosion resistance, protecting the chain from wear, rust, and damage even in harsh industrial conditions. This results in extended service life and reduced maintenance costs.
Q: Where can I utilize this elevator bucket chain?
A: This chain is ideal for installation in rice mills, grain handling facilities, flour mills, and any other industrial unit that requires reliable bulk material handling equipment.
Q: What is the process for ordering and receiving the product?
A: To order the MS Elevator Bucket Chain, simply contact us with your requirements. Upon finalizing the proposal amount, we process your order, handle packing and shipment, and offer FOB from major Indian ports for prompt delivery.
Q: When should I consider replacing my elevator bucket chain?
A: Replace your chain when you observe signs of extensive wear, elongation, or surface corrosion, or during scheduled maintenance intervals to ensure optimal performance and prevent downtime.
Q: How does the chain's heavy-duty capacity benefit my operation?
A: Its heavy-duty design enables efficient handling of large quantities of materials, minimizing operational delays and increasing overall productivity in bulk handling processes.
 Send Inquiry




 Send Inquiry


 Send Inquiry
